How to Choose the Best Polyimide Tape for Your Needs?
Choosing the best polyimide tape is rarely as simple as selecting the highest temperature rating. Real performance depends on the application, surface, adhesive, and working environment. A tape used for circuit-board masking may need clean removal, while one wrapped around a motor coil must resist heat, voltage, and mechanical stress. The right choice begins with understanding what the tape must endure every day.
Experienced technicians usually examine temperature exposure, dielectric strength, thickness, tensile strength, and adhesive behavior. They also consider whether the tape will contact silicone, metal, plastics, or rough insulation. A thin film can fit tight spaces, but it may tear during installation. A thicker grade offers better handling, yet it can affect clearances. Small details matter.
Do not trust one specification alone. Test a sample on the actual surface whenever possible. Leave it under expected heat, then inspect the edges, residue, and bond strength. This practical step often reveals problems that a product sheet cannot show. Certification and supplier traceability also support safer decisions, especially in electrical and aerospace-related work. Still, product claims require careful verification. Even experienced buyers can overlook humidity, repeated movement, or rushed application. There is no universal best tape. There is only the most suitable choice for a clearly defined need.
What Is Polyimide Tape and How Does It Work?
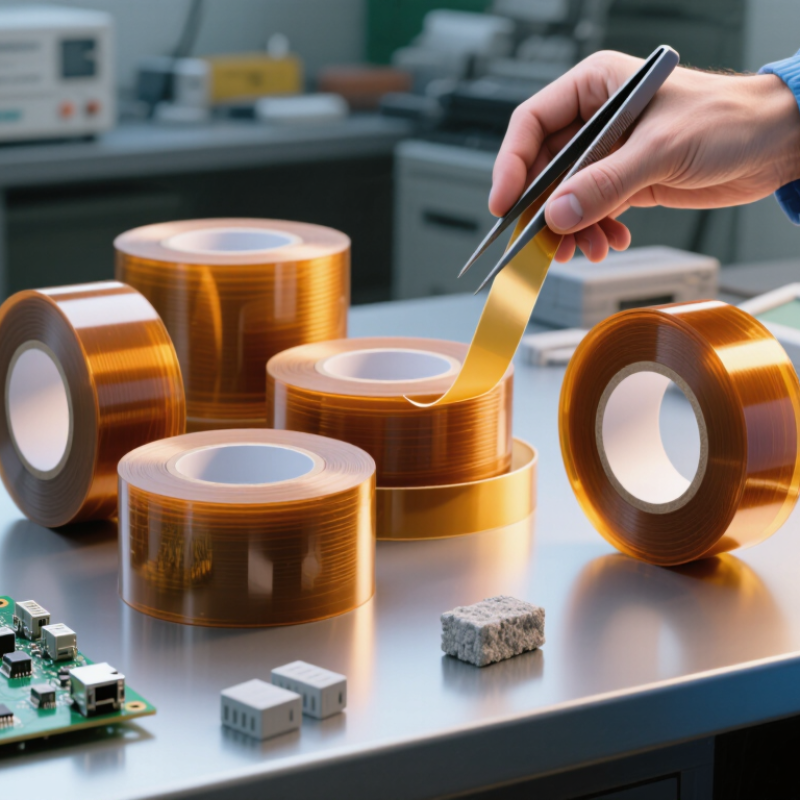
Polyimide tape is a thin adhesive tape built around a polyimide film. This amber-colored film stays stable under heat, electrical stress, and repeated handling. Its adhesive layer bonds to surfaces without greatly changing the tape’s shape. When wrapped around wires or placed over circuit areas, the tape creates insulation and protects against solder splashes, abrasion, and short-term heat exposure.
The tape does not work by heat resistance alone. The adhesive must remain attached without leaving heavy residue. Its performance depends on temperature, pressure, surface cleanliness, and exposure time. A clean metal or polymer surface usually gives better bonding. In practical work, I press the tape firmly with a smooth tool and inspect the edges for lifting. A common mistake is choosing the thickest tape automatically. Thick tape can reduce flexibility and create unwanted steps around small components. I also check whether the adhesive is silicone-based or acrylic-based, because removal behavior may differ.
Tips: Match the tape to the real working temperature, not the equipment’s advertised maximum. Test a small piece first. Check insulation needs, thickness, width, and residue after heating. If the tape will bend repeatedly, evaluate flexibility after installation. I have found that quick visual checks can miss weak corners, so gentle pull testing is useful. Still, this test is not a substitute for documented technical data. Temperature ratings can be misunderstood. Always confirm the film and adhesive limits separately.
Which Performance Factors Matter for Your Application?
When choosing polyimide tape, temperature rating is only the starting point. The adhesive must survive your real process, including heating speed, dwell time, pressure, and removal. A 2023 reliability review from the U.S. National Renewable Energy Laboratory reports that power-electronics components may experience operating temperatures near 150–200°C. That range can quickly expose weak adhesive systems.
Electrical insulation also deserves close attention. Check dielectric strength, insulation resistance, and thickness consistency. ASTM D1000 provides recognized methods for measuring adhesion, tensile strength, and elongation. These tests help compare samples under controlled conditions. However, laboratory values may not match a dusty assembly line. I would test the tape on the exact substrate, especially textured plastics or powder-coated metal.
Mechanical performance matters during cutting and masking. A tape that stretches too easily may wrinkle around sharp corners. Excessive adhesion can leave residue after a long thermal cycle. For circuit protection, verify flame behavior and insulation requirements against the applicable safety standard, such as UL 510. Do not rely on a single headline value. A 2024 industry analysis of high-temperature electrical materials links demand growth to electrification and compact electronics, but market forecasts cannot replace application testing. Small details matter. Test peel strength after heat exposure, humidity conditioning, and repeated removal. My own practical mistake would be choosing the strongest adhesive first; clean release can be more valuable than maximum grip.
How to Compare Quality, Cost, and Supplier Reliability?
Choosing polyimide tape starts with the application, not the lowest quotation. Check temperature, voltage, insulation needs, and surface condition. In production, I have seen tape fail because its adhesive softened near a heater. Ask for measured data, including continuous temperature ratings, dielectric strength, thickness tolerance, and peel adhesion. Request samples. Apply them to the actual substrate, then inspect the edges after heating and cooling. A clean release matters. So does residue.
Cost comparison should include labor, waste, and replacement risk. A cheaper roll may have uneven coating or inconsistent winding. That creates wrinkles, torn liners, and slower assembly. Compare the price per usable meter, not the price per roll. Review batch records and certificates before approval. Independent test reports can support supplier claims, but they do not replace your own trial. Check packaging, storage guidance, lead times, and response speed. A supplier who answers technical questions clearly is easier to trust. Still, friendly emails do not guarantee reliability. Keep evidence.
Tips: Build a simple scorecard. Give quality, cost, and delivery separate weights. Test at the highest realistic temperature. Record lot numbers and failure photos. Ask how complaints are investigated and corrected. Avoid choosing from one sample alone. That was my mistake once. Do not ignore details like roll telescoping or adhesive transfer. They often become expensive during full-scale production.
How to Choose the Best Polyimide Tape for Your Needs?
Compare quality, cost, and supplier reliability by first matching the adhesive system to the required operating temperature.
The chart shows representative continuous-use temperature limits commonly published for generic polyimide tapes: silicone adhesive up to about 200°C, acrylic adhesive up to about 150°C, and rubber adhesive up to about 80°C. Actual performance depends on tape thickness, adhesive formulation, dwell time, pressure, substrate, and test method. For purchasing decisions, verify technical data, request samples and lot certificates, compare total cost per usable roll, and assess supplier reliability through lead-time consistency, quality-control records, and production capacity.